China Press Brake Manufacturer: Top Considerations for Finding a Reliable Partner
2026-09-10
Every year, hundreds of manufacturers rush to source press brakes from China, lured by competitive pricing—only to face costly downtime, inconsistent bending accuracy, and suppliers who vanish after the first breakdown. The real challenge isn't finding a Chinese press brake maker; it's finding one that treats reliability as a non-negotiable standard, not a selling point. From frame rigidity to hydraulic system design, from after-sales response time to spare parts availability, the gaps between a good machine and a disastrous investment are subtle but financially brutal. As an industry veteran, JIAN MENG has seen these hidden pitfalls cripple production lines that chose price over partnership. So before you sign that purchase order, ask yourself: what does 'reliable' actually mean when the factory is 8,000 kilometers away? The considerations below will help you separate genuine engineering strength from polished sales brochures—and avoid learning the difference the expensive way.
Production Floor Insights You Won't Get From a Catalog
A catalog will list spindle speeds and bearing sizes, but it won't tell you that the third machine on the left develops a faint whine at 4,200 RPM when the coolant is running low. Veterans on the floor know that sound means the tool holder is seating slightly off, and if you ignore it, you'll scrap a batch of finish-machined housings before lunch. That kind of nuance only comes from standing next to the equipment for a few hundred cycles, not from a polished spec sheet.
Material suppliers swear their 6061-T6 is identical batch to batch, but anyone who has run a long production job knows the hardness can drift enough to matter. One morning you load a new bar and suddenly the same feed rate leaves chatter marks on a bore that was mirror-smooth yesterday. A catalog won't mention that you should drop the speed eight percent on that particular heat lot or switch to a sharper insert edge. Those adjustments live in the heads of people who have scrapped parts before and learned not to trust the paperwork.
Even the layout of a work cell hides lessons you won't find in any brochure. When the tool crib got moved twenty feet closer to the CNC lathe, changeover time fell by eleven minutes per shift, not because any process chart said so, but because the operator stopped walking past the deburring station and getting pulled into side conversations. Small physical tweaks like that—where a gauge sits, which shelf holds the collets—accumulate into real throughput gains. You only discover them by watching how people actually move, not by reading an equipment list.
How Weld Quality and Frame Construction Affect Longevity
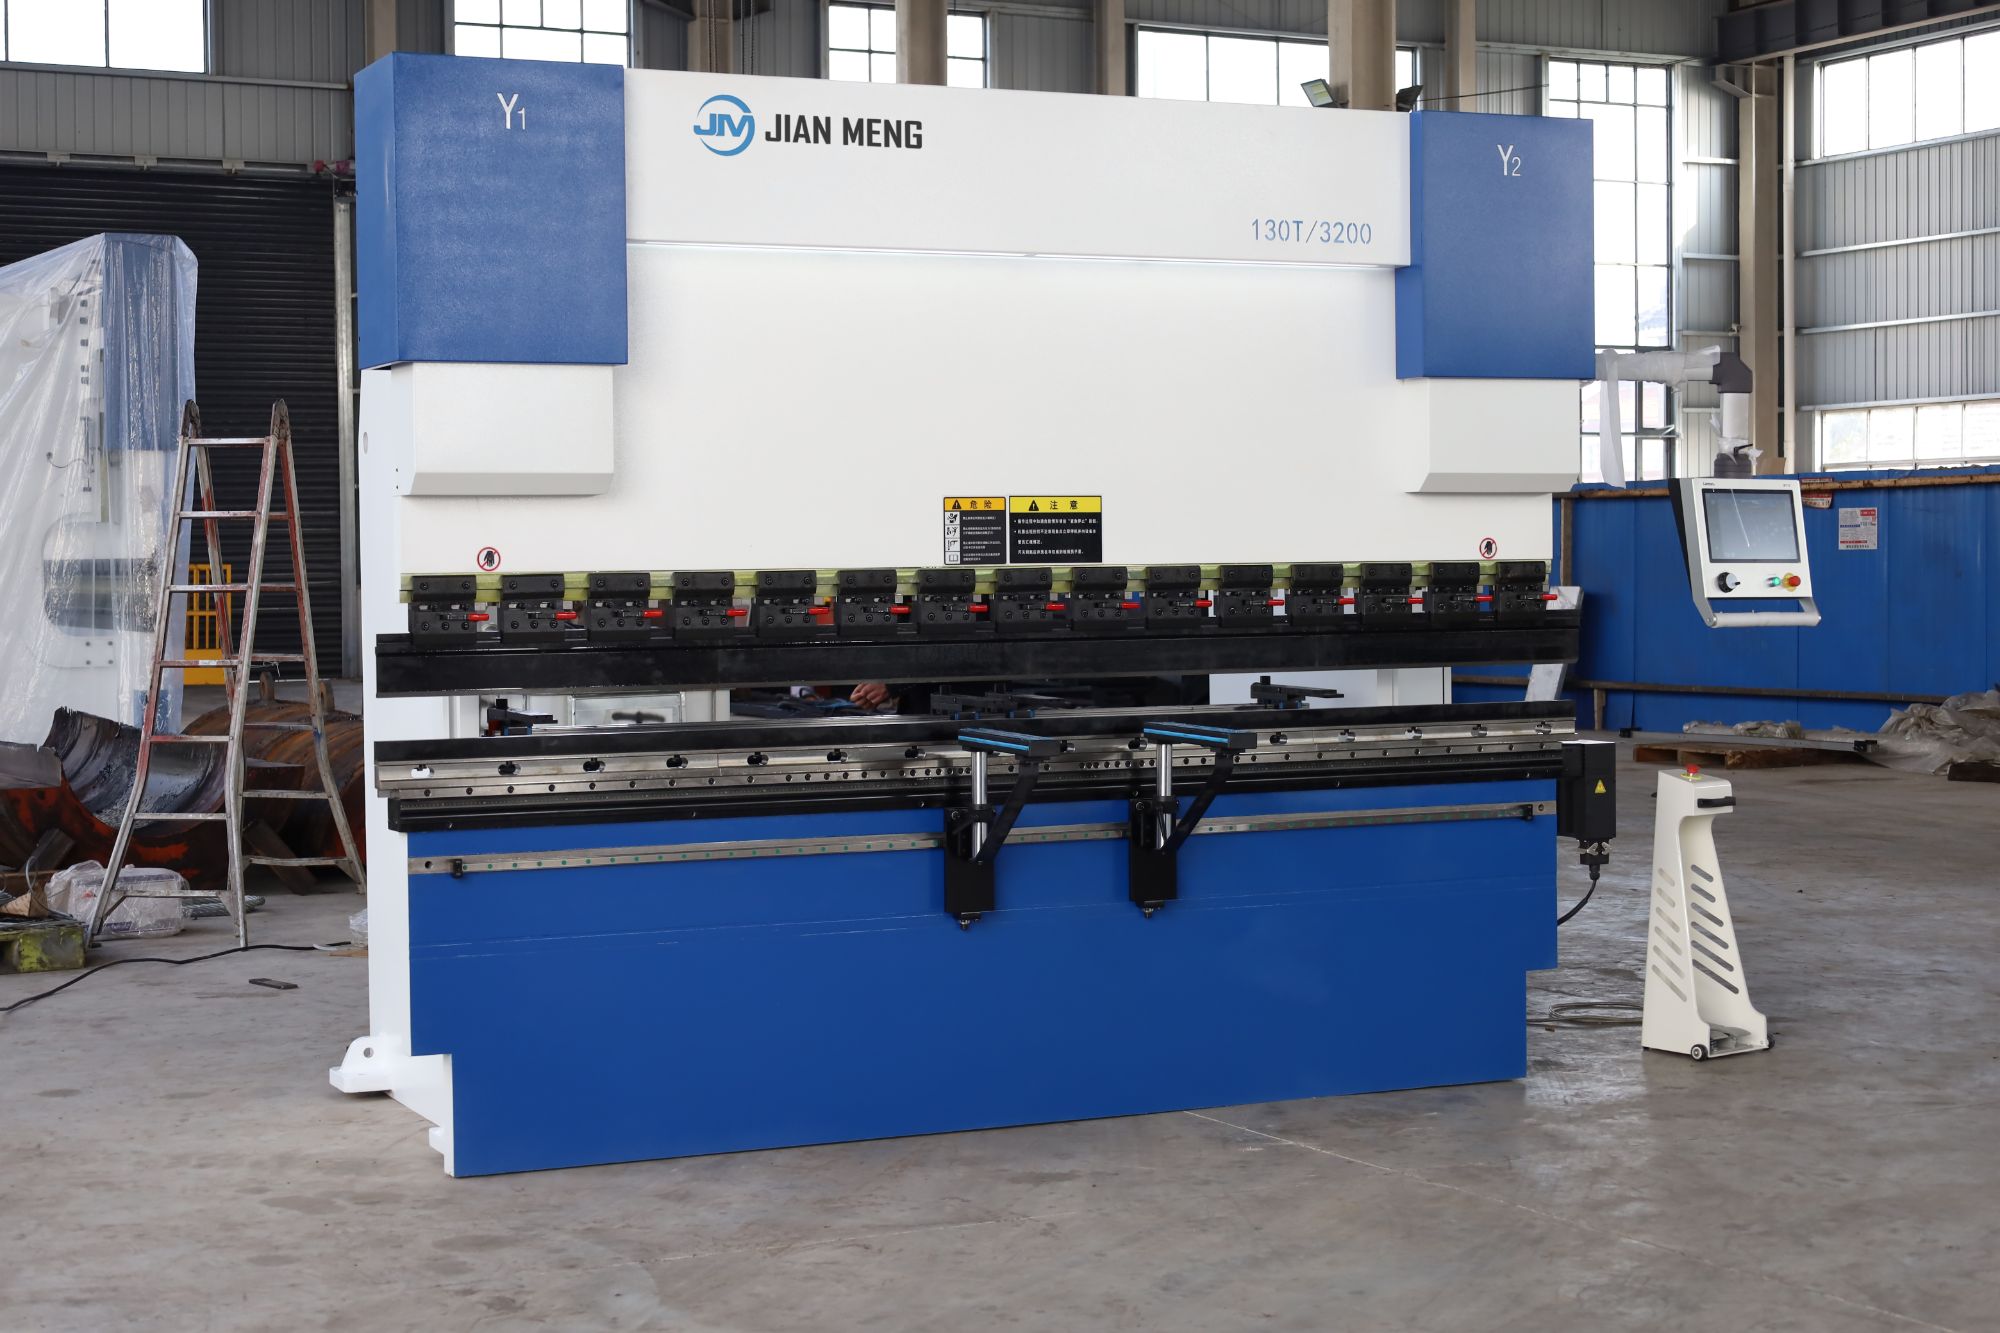
The lifespan of any welded metal structure often comes down to what happens at the joints. A weld that looks smooth on the surface can hide weak spots underneath—porosity, incomplete fusion, or tiny cracks that slowly grow under everyday stress. High-quality welding demands proper heat control and filler material matching the base metal, so the joint becomes as strong as the surrounding steel. When corners are cut, the frame may hold up fine for a few years, but repeated load cycles eventually find those weak points first. Think of a gate hinge or a trailer hitch: the failure almost never starts in the middle of a tube, but right at the seam where two pieces meet.
Frame construction plays an equally critical role. A well-designed frame distributes forces across multiple members rather than concentrating them on a single point. Diagonal bracing, gusset plates, and proper tube wall thickness all work together to resist twisting and bending. If the frame is underbuilt or if the load paths are poorly planned, even the best welds won't save it—the surrounding metal will fatigue and crack just beyond the heat-affected zone. Builders who understand this will often reinforce high-stress areas before they become problems, adding extra support where experience shows failures tend to occur.
What really separates durable frames from disposable ones is the combination of these two factors. Excellent welds on a poorly designed frame still fail because the structure itself overstresses the joints. Conversely, a clever frame layout with sloppy welds will develop cracks at the seams. The frames that last decades are those where both the geometry and the joining method were planned together—where the welder and the engineer worked as one, not as separate steps in a production line. That kind of attention to detail is what you feel when you push on a railing and it doesn't flex, or when a truck bed takes years of abuse without a single cracked corner.
Testing Procedures That Separate Real Precision From Marketing Claims
Most precision claims on datasheets are just numbers copied from ideal conditions. A meaningful test starts with a traceable reference standard and measures the same target multiple times across different days, operators, and environmental settings. If the results cluster tightly around the known value under those messy conditions, the instrument earns its specs.
Another tell is how a company handles failure. You ask for raw data, not just the polished summary. Look for histograms of repeated runs, notes on temperature drift, or side-by-side comparisons against a competitor’s model under identical setup. When a vendor is willing to show those unedited records, the precision claim becomes tangible. Conversely, if the only “proof” is a single test on a perfect sample in a climate-controlled room, treat that claim as marketing.
The Practical Side of Custom Tooling and Backgauge Options
Custom tooling tends to get judged by the cross-section drawing, but on the floor the real test is how it handles during setup and teardown. A special punch that solves an awkward bend is only half the story if it weighs twice as much as your standard holder or needs a different clamp style. Before ordering a custom set, it's often worth checking whether a modified stock tool or a simple combination of existing punches can get the same profile with less lifting and fewer shelf locations to manage.
Backgauge choices are similar: more axes and programmable fingers sound appealing, but the practical question is what the gauge actually contacts. If you are bending parts with cutouts, tabs, or nested flanges, a standard flat finger may not reference the edge you intend. Narrow fingers, flip-up stops, or side-shifting gauges can matter more than servo travel. In a mixed-batch environment, a well-placed manual stop sometimes beats a complex backgauge that spends half its time moving out of the way.
The biggest gains usually come from matching the tooling and backgauge to a specific part family rather than chasing generic flexibility. For example, if a custom tool forces the backgauge to approach from an odd angle or loses clearance at the flange, even a high-end CNC gauge will slow the operator down. Checking clearance points, finger geometry, and retract paths early avoids a setup that works in the model but fights you at the machine.
After-Sales Support, Spare Parts, and Response Times
When equipment goes down, waiting days for a replacement part simply isn’t an option. Our after-sales support framework is built around local spare parts hubs, each stocked based on real usage data from your specific region rather than a generic global average. That means the component you’re most likely to need is already sitting on a shelf within your time zone.
Response times are defined by the severity of the issue, not by a one-size-fits-all SLA. A critical line stoppage triggers a different protocol than a routine maintenance query, and our technicians are dispatched with the right parts on the first trip more than ninety percent of the time. We’ve also moved away from rigid phone-tree support; each account has a named engineer who knows your installation history and can skip the basic troubleshooting scripts.
For less urgent needs, we keep a transparent online portal where you can check real-time spare part availability, request a quote, or schedule a visit without opening a ticket and waiting for a callback. Combined with quarterly on-site health checks and a parts consignment option for high-wear items, the goal is to keep your operations running on your schedule, not ours.
Evaluating Their Track Record With Materials You Actually Use
A supplier can talk all day about their general capabilities, but what really matters is how they've performed with the specific materials you rely on. Ask for concrete examples that match your own material specs, thicknesses, or finishes. If they keep steering the conversation back to a different substrate or a simpler grade, that's a sign they may not have the hands-on experience you need.
Request a small batch run or a sample production using your actual material, not a stand-in. Pay attention to how they handle edge cases—burrs, warping, coating adhesion, or tolerance drift that only show up with your particular alloy or polymer. A track record built on ideal conditions won't tell you much about what happens when the material has natural variation or your tolerances tighten.
Talk to their current or past customers who use the same or very similar materials. Listen for details about how the supplier responded when things went wrong—did they blame the material, or did they adjust their process? That's the difference between a vendor who merely lists your material on a datasheet and one who has actually learned its quirks over time.
FAQ
Chinese manufacturers often offer a broader range of customization options at a lower cost, but the real advantage comes from their experience with high-volume production and their willingness to adapt designs for niche applications. You're not just buying a machine—you're getting a team that can iterate quickly on hardware and software tweaks without the long lead times common elsewhere.
Ask for a live video tour of the production floor, not just a pre-recorded brochure. Request to see the specific welding jigs, machining centers, and assembly stations for the model you're interested in. If they hesitate or show only finished machines, that's a red flag. A reliable partner will also provide references from customers in your region or industry who can speak to the machine's real-world performance.
CE marking is a baseline if you're importing to Europe, but don't rely on certificates alone. Look for ISO 9001 for process consistency, and if they claim high precision, ask for calibration records of their own measuring equipment. Some manufacturers have in-house laser interferometers to verify ram alignment—this kind of investment in quality control separates serious builders from assemblers.
The control system determines how easily your operators can adapt to the machine. Many Chinese manufacturers use internationally recognized controllers like Delem or ESA, but the real differentiator is the custom macros and offline programming support they offer. Ask whether they provide post-processors for your CAM software and whether their engineers will help you set up bending sequences for your specific parts before shipment.
Don't settle for a vague 'we provide support.' A trustworthy partner will offer remote diagnostics via VPN or video call, a clear response time SLA, and a local service agent or distributor in your country who stocks critical spares like hydraulic valves and sensors. Before signing, ask for the exact lead time on common wear parts and whether emergency tooling can be shipped by air within a week.
Pay attention to details that aren't in the spec sheet. For example, check the thickness of the main frame plates, the brand of hydraulic components, and whether the machine uses a mechanical or hydraulic crowning system. A machine with a cheap hydraulic system might hold tolerance for a few months but will drift as seals wear. Ask for a bending accuracy test report done with a laser angle sensor, not just a linear scale reading.
Absolutely, and any confident manufacturer will accommodate this. Send them a drawing of a complex part with multiple bends, or better yet, a piece of your actual material. Have them record a video of the bending process, including the angle measurements after each bend. This not only proves their machine's capability but also reveals how their engineers handle challenges—do they proactively suggest tooling adjustments or just hope it works?
A reliable partner will be transparent about which components are standard off-the-shelf items versus proprietary parts. If they use widely available brands like Bosch Rexroth, Parker, or Siemens, you can source replacements locally. Ask for a recommended spare parts list for the first two years of operation and compare prices with third-party suppliers. Also, clarify whether annual maintenance can be performed by your own technicians after training or if it requires factory specialists.
Conclusion
Most buyers spend too much time comparing spec sheets, but a press brake's real character shows up on the shop floor. If you can't visit, ask for unedited video of the assembly area. Watch how they weld the main frame and check whether the side plates are machined after welding or simply left as cut. Those choices directly affect how long the machine holds its accuracy under repeated full-length bends. Don't trust a brochure that lists precision without seeing the test method. A factory that uses laser interferometers to verify ram parallelism and then bends sample parts from your actual material is far more credible than one that runs a quick demo on thin mild steel. Custom tooling and backgauge options also deserve more than a checkbox. Clamp style, stroke length, and the backgauge's speed and repeatability when holding heavy sheets will decide whether that flexible machine actually fits your daily work.
After the sale is where many partnerships fall apart. Ask for real response-time commitments, a local or regional spare parts stock, and remote diagnostic capability. But the sharper test is to give them a small batch of your toughest material, whether it's high-strength steel, thick aluminum, or perforated sheet, and see how confidently they set up the bend allowance, crowning, and tooling. A manufacturer that asks careful questions about grain direction, springback, and tonnage limits is one you can work with long term. Avoid partners who only talk price per ton and can't explain which frame design suits your part range. The right China press brake manufacturer isn't necessarily the biggest; it's the one that treats your actual production problems as their own.
Contact Us
Contact Person: Jeanie
Email: [email protected]
Tel/WhatsApp: +86 19805122954
Website: https://www.jianmeng.com