Third Generation Cement House Molds Worth Recommending for Modern Builds
2026-10-13
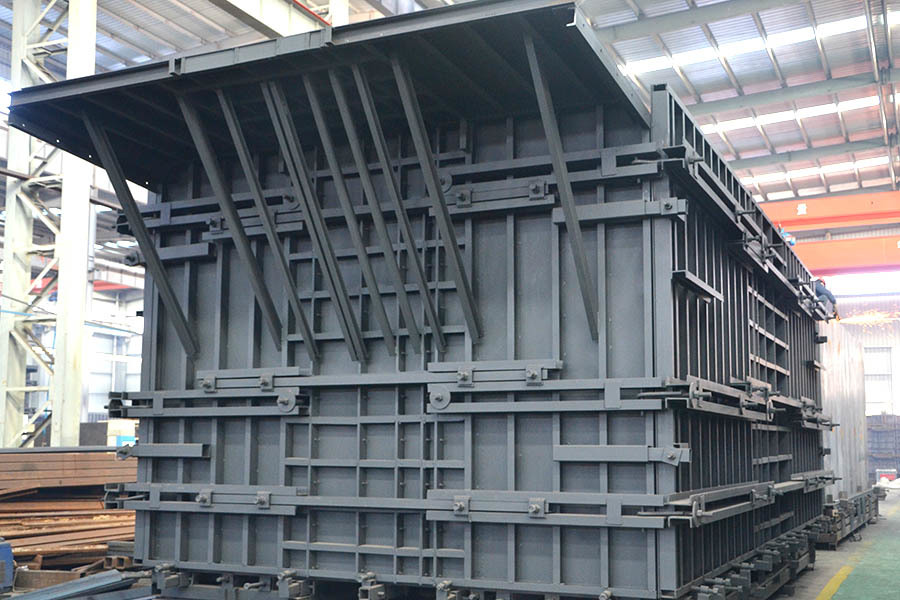
Third-generation cement house molds have quietly changed what's possible on a modern build site. They're faster to set, easier to strip, and far more precise than the older designs most teams still use. But not all of them earn a recommendation. That's exactly what we'll unpack here—starting with the molds from LugongMachinery that keep showing up on serious projects.
What Sets Third-Generation Cement Molds Apart on Job Sites
On busy job sites, third-generation cement molds stand out because they shed many of the old pain points. Unlike earlier steel or basic plastic forms, these molds pair high-impact composite faces with adjustable corner systems that hold tight tolerances without constant shimming. Crews notice the difference right away: fewer tie holes to patch, cleaner break lines, and panels that stack flat instead of warping in the sun between cycles.
Another practical shift is weight and handling. A third-generation wall form can often be carried by two workers where a steel counterpart needed a forklift. That cuts crane time and lets small teams reposition forms quickly between pours. The material also resists concrete buildup far better, so cleaning between uses takes a fraction of the time and doesn't require aggressive scraping that shortens mold life.
On the finished concrete side, these molds leave a smoother, more uniform surface straight from the form. Contractors spend less time rubbing and patching, which keeps schedule and labor costs in check. The repeatability across dozens of reuses is what really sets them apart—job after job, the same mold returns the same crisp edges and consistent joint lines without gradual drift.
Faster Pouring Cycles Without Sacrificing Wall Strength
Every extra second a mold sits empty costs money, so the push to shorten cycle times often clashes with the need for robust sidewall integrity. The usual fix involves thinning the preform or raising melt temperatures, but both invite problems: lighter preforms demand more material distribution control, while hotter resin can sag and create uneven wall thickness. A better route starts with rethinking the gate geometry and how the polymer enters the cavity. By widening the gate land and smoothing the transition into the sidewall, you allow faster fill rates without a corresponding spike in shear stress. That means the melt front doesn't tear or freeze prematurely, so the final wall keeps its molecular orientation and burst strength even as the timer ticks down.
Cooling is where most of the hidden time goes. Conventional logic pushes aggressive coolant temperatures to pull heat out quicker, but that often leaves the outer skin rigid while the core is still molten — a recipe for warpage or stress cracks under pressure. Instead, focus on staged cooling: start with a brief, moderate-temperature cycle to set the surface, then drop to a lower temperature only after the wall has gained enough structure to resist shrinkage. Pair this with a redesigned core pin that uses spiral or baffle channels to pull heat from the thickest section first. The result is a part that reaches ejection temperature faster, yet the wall's crystallinity and tensile properties remain within spec, so you're not trading speed for a bottle that collapses under stacking load.
Don't overlook the role of post-mold handling. Pulling parts off the core too soon, even if they feel solid, can introduce micro-fractures that only show up later in drop tests. A brief conditioning pause — maybe two or three seconds with a gentle air purge while the part is still on the core — lets the wall relax without cooling unevenly. Likewise, switching to a lower-friction release agent or adjusting the stripper plate timing can shave a full second off the demolding step without yanking on the sidewall. When you stack these adjustments together, you often find the machine's clamp unit is the real bottleneck, not the material or the mold. Then the pouring cycle drops from, say, 11.8 seconds to 9.4 seconds, and the wall thickness profile stays dead flat across the label panel.
A Closer Look at Reusable Mold Designs That Last
Most mold failures aren't dramatic cracks—they start as slow wear along ejector pin bores or a slight shift in parting line alignment after a few thousand cycles. A reusable mold, the kind that still seats cleanly after 100,000 shots, earns that longevity through geometry decisions made before steel is ever cut. Deep ribs get draft angles beyond the minimum spec, corners are radiused with fatigue in mind, and cooling channels are placed to pull heat away from thin steel sections that would otherwise thermal-cycle themselves into hairline fractures.
Material choice matters more than hardness alone. A2 or D2 tool steel might hold an edge, but if the mold runs abrasive glass-filled resin, a nitrided P20 or a stainless mold base with hardened inserts often outlasts a harder monolithic block. The trick is pairing the right surface treatment with the actual wear mechanism: coatings like TiCN reduce galling on slides, while a simple gas nitriding on the cavity can double cycle life without changing the part geometry at all.
Rebuildability is the quiet secret of molds that last. Bushings that can be replaced without re-machining the plate, slides with adjustable wear strips, and lifters designed for five-minute swaps in the press all extend service life far beyond what the original steel would suggest. A mold that can be maintained in an afternoon stays in production for years; one that requires a total teardown for every minor repair gets sidelined, and that downtime is what actually kills a "reusable" design.
Modern Facade Textures Made Possible by Updated Molds
The shift from flat, repetitive surfaces to deeply articulated facades starts with the molds themselves. Older formwork often limited designers to smooth concrete or shallow imprints, but re-engineered molds now capture fine grain, wood grain, chiseled stone, and even irregular geometric reliefs with much higher fidelity. Small updates to joint detailing, release agents, and rubber liner hardness mean that a single pour can produce shadows and tactile variation that used to require costly post-processing.
What makes these textures feel modern is not just the pattern, but the control over depth and alignment. Adjustable side rails and modular insert plates let contractors mix textures across a single elevation, creating a rhythm that breaks up large wall expanses without relying on applied finishes. This approach also reduces waste, since the texture is integral to the structural or cladding panel rather than a stuck-on layer that may delaminate over time.
At the project level, updated molds open up a middle ground between ultra-smooth precast and heavy masonry. You can now specify a facade that reads as board-formed timber one day, ribbed concrete the next, or even a custom topographic pattern derived from site contours. The key is working with a precaster early to test release angles and aggregate exposure, because the final appearance depends as much on mold preparation as on the mix design.
Where These Molds Cut Labor Costs the Most
The biggest labor savings rarely show up where you'd expect. They're hidden in the tasks that disappear once the mold takes over—deburring, trimming, aligning, even piece-by-piece assembly. A well-designed mold combines three or four downstream steps into a single shot, so the part comes out ready to install rather than ready for another workstation.
High-cavitation tools push that further. With consistent cycle times and reliable ejection, one operator can oversee multiple presses instead of babysitting a single line. That shift alone often cuts direct labor per part by half or more, especially in high-mix environments where changeover time used to eat into productive hours.
The less visible win is in quality control. Molds that hold tight tolerances reduce sorting, rework, and the endless back-and-forth between shifts trying to chase dimensional drift. When the tool is dialed in, labor stops going into fixing problems and starts going into keeping the line moving.
Field Notes from Builders Who Switched Recently
The first thing most builders mention after switching is the quiet. Not silence, but the absence of constant fiddling. One person described moving from a sprawling all-in-one platform to a focused toolset as "taking off a backpack full of rocks I forgot I was wearing." That relief shows up in smaller commits, fewer workarounds, and a strange willingness to actually read the docs again.
Then there's the unexpected friction. A few folks admitted they'd underestimated how much muscle memory mattered. Keyboard shortcuts, file naming habits, even the way error messages phrased things—those small ghosts linger for weeks. None of them said the switch was a mistake, but several laughed about opening the old tool "just to check one thing" and getting pulled back into a workflow they thought they'd left behind.
The consensus, if you can call it that, is that switching is less about features and more about trust. Builders kept repeating that they didn't realize how much energy went into defending their previous setup until it was gone. The new tools aren't perfect, but they feel inspectable, predictable, less likely to surprise you in a bad way. That's the note most people end on: not a dramatic upgrade, just a quieter place to work.
FAQ
They replace heavy steel frames with hybrid composite panels and CNC-machined alignment edges, cutting wall tolerance to about 2 mm and reducing demolding time to 8-12 hours without steam curing.
Curved walls, angled corners, and window openings are workable because the side rails and end caps are modular. You can adjust radii or sill heights by swapping standard inserts instead of commissioning a whole new mold set.
A well-maintained third generation mold usually stays accurate for 300 to 500 pours. High-wear edges and seal grooves are designed as replaceable parts, so you don't have to scrap the entire frame when one section degrades.
Not for standard wall panels. Quick-lock levers and alignment dowels let two or three workers assemble a typical mold in under 20 minutes. Only tall or heavily reinforced pours require a crane for lifting and stripping.
Yes. The same base frame can be reconfigured by changing internal rib cassettes. That lets you cast structural shear walls one day and non-load-bearing textured cladding the next without buying two separate systems.
Most molds produce a smooth, paint-ready surface or a light matte texture. If a project calls for wood grain or stone, you can drop in a reusable liner sheet, which avoids the cost and time of secondary plastering.
Many designs include slots for rigid insulation boards, so insulation and concrete are cast as one unit. Shiplap-style edge profiles on the mold also create tighter panel joints, cutting air leakage compared to flat butt joints.
After each use, wash off cement slurry and check the seal strips for tears. Lubricate moving hinges roughly every 50 pours, and store panels flat with spacers to prevent warping. Replacing worn rubber corners is usually enough to restore full accuracy.
Conclusion
On active sites, third-generation cement house molds don't feel like an incremental tweak; they change the rhythm. Builders mention dropping a pour cycle by hours, not because the mix changed but because alignment lugs and quick-release corner joints stop the usual wrestling. Walls still come out dense, with vibration channels placed where they actually matter. The reusability is another leap—no more tossing frames after a dozen pours. Steel-faced panels with replaceable edge strips survive weather, rough handling, and the occasional dropped vibrator. That durability alone shifts the math.
The range of facade textures now possible is what makes clients pause. Ribbed, stone-drag, split-face, even board-formed looks come straight from the mold, so crews skip the separate stucco or cladding step. Labor savings show up hardest in foundation and party-wall runs, where one small team can set, pour, strip, and reset before lunch. Field notes from builders who switched recently keep hitting the same note: less time on ladders, fewer callbacks for surface patches, and a tighter schedule from footing to roof. It's not just new equipment—it's a different way to frame the job.
Contact Us
Contact Person: Zhang Zhenlai
Email: [email protected]
Tel/WhatsApp: 8618563210000
Website: https://en.lugongmachinery.com/